


Injection molding
Custom injection molded parts.
- Price matched to the part’s use, to give you the best price
- Mold in aluminum or hardened steel
- Samples before production
- Every shot comes out of that same mold
Your parts protected by an NDA.
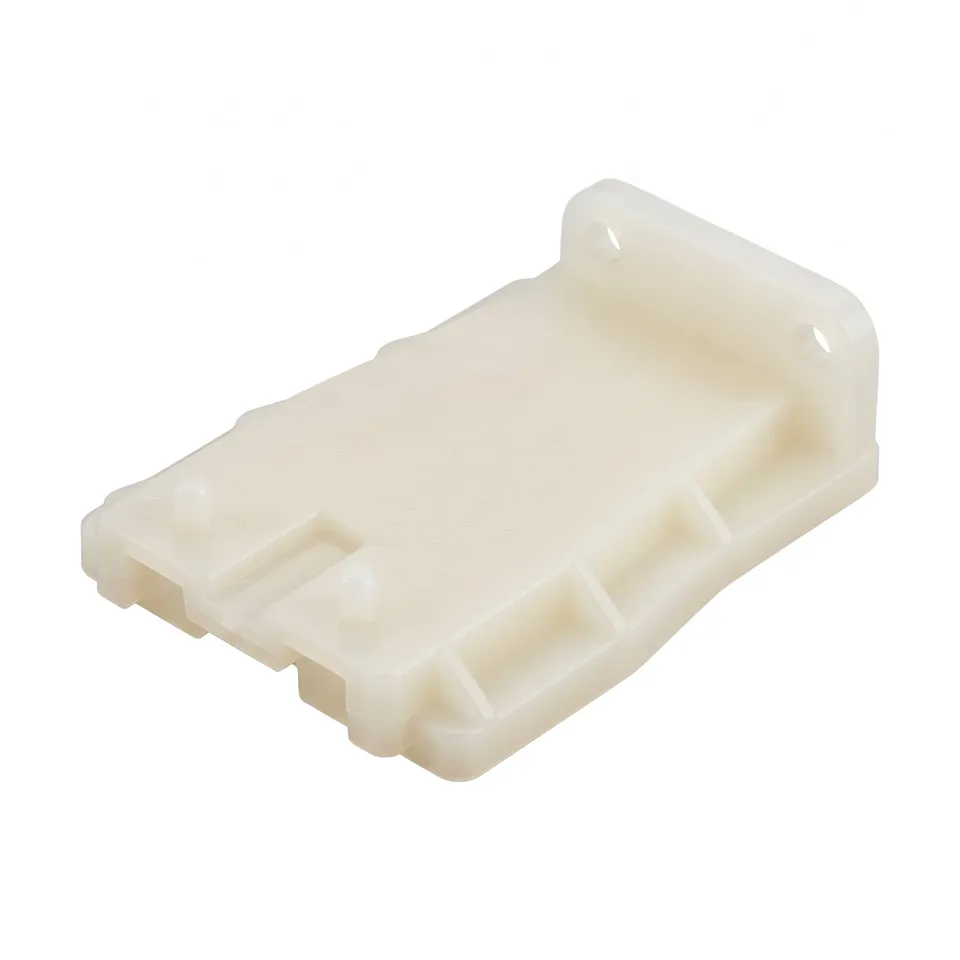
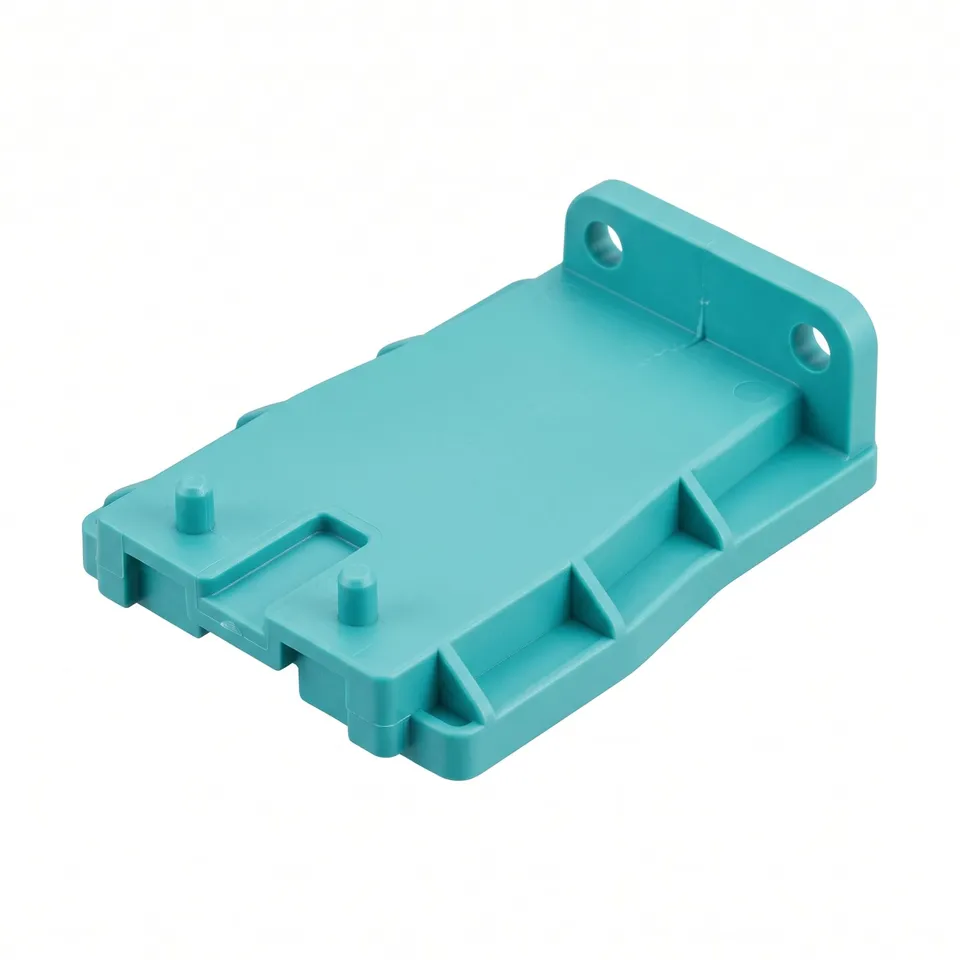
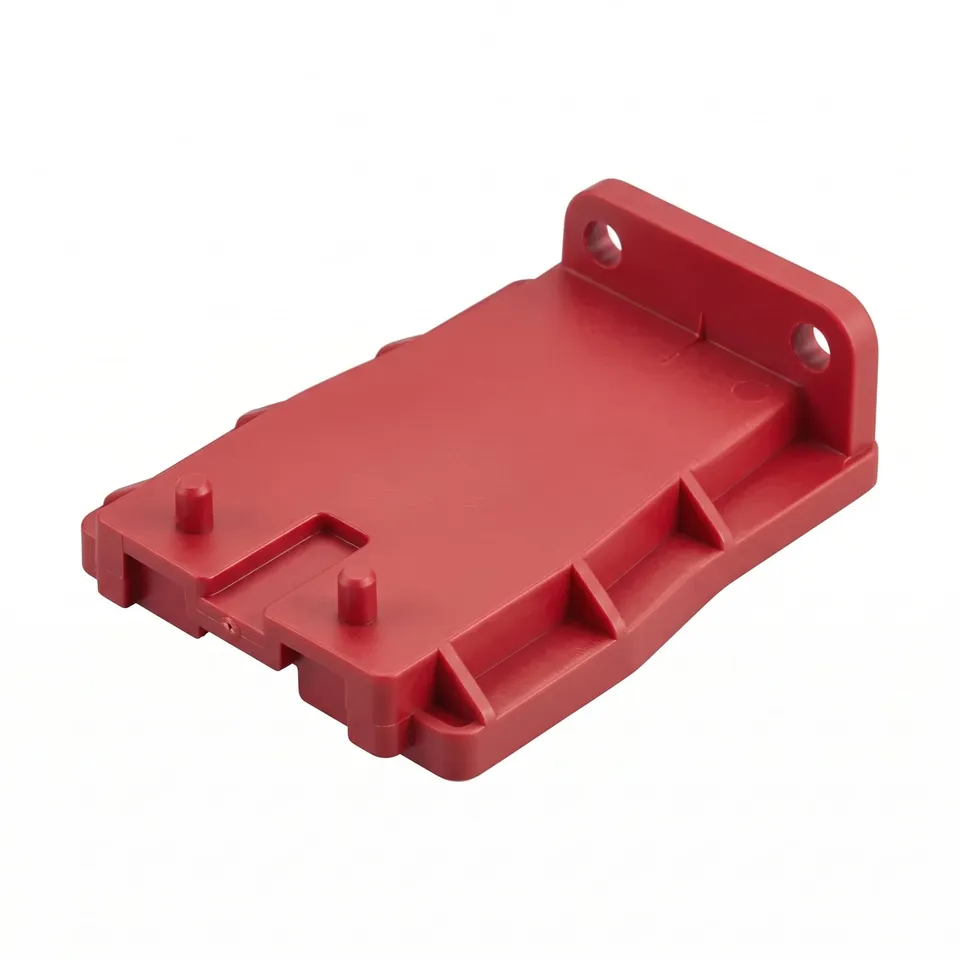
- Injection molding
Everything from the first shot to the last.
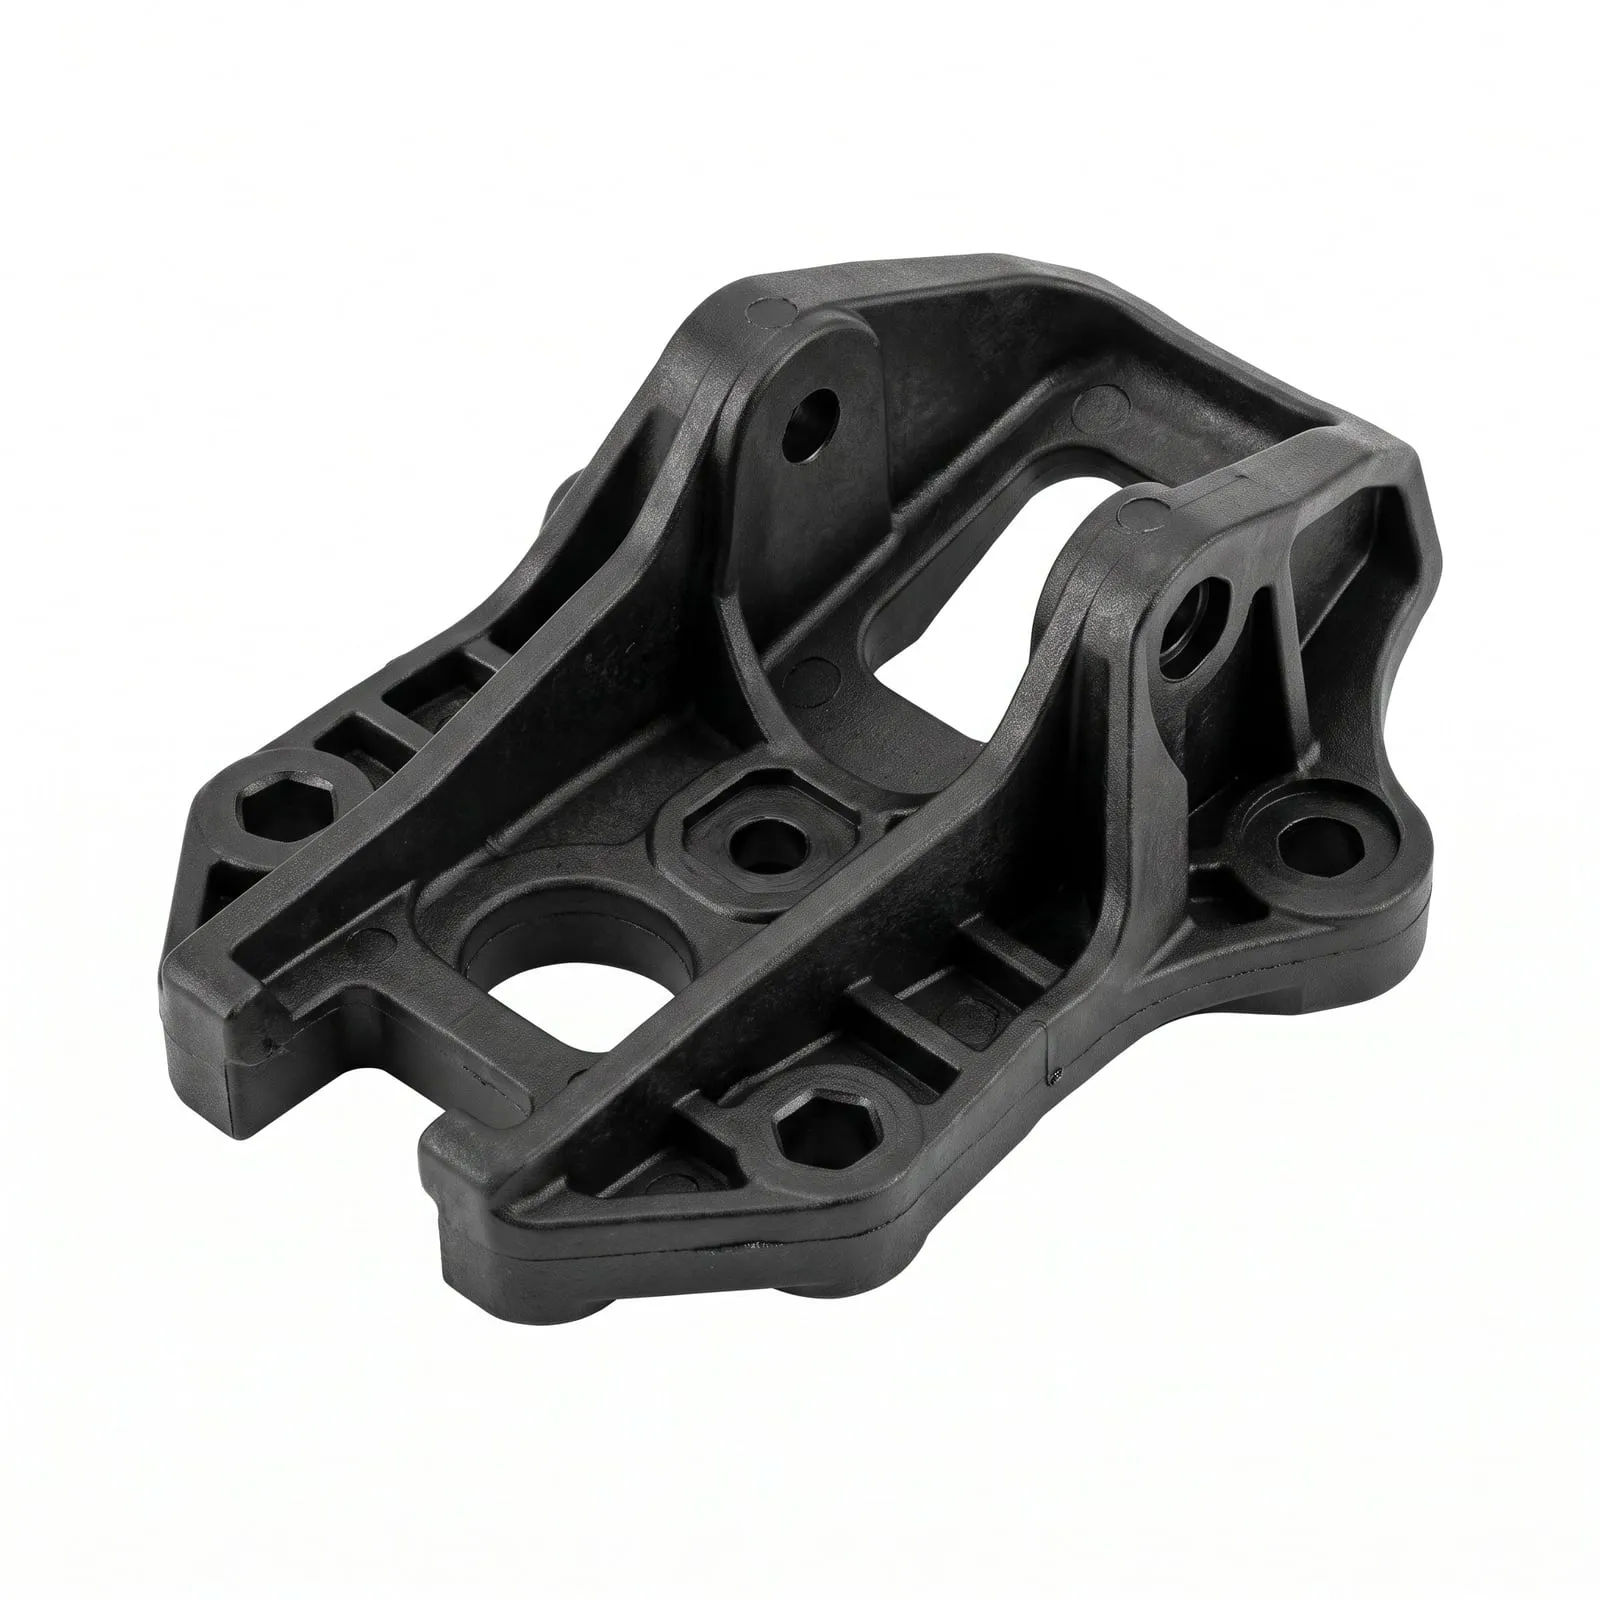 Draft and walls checked
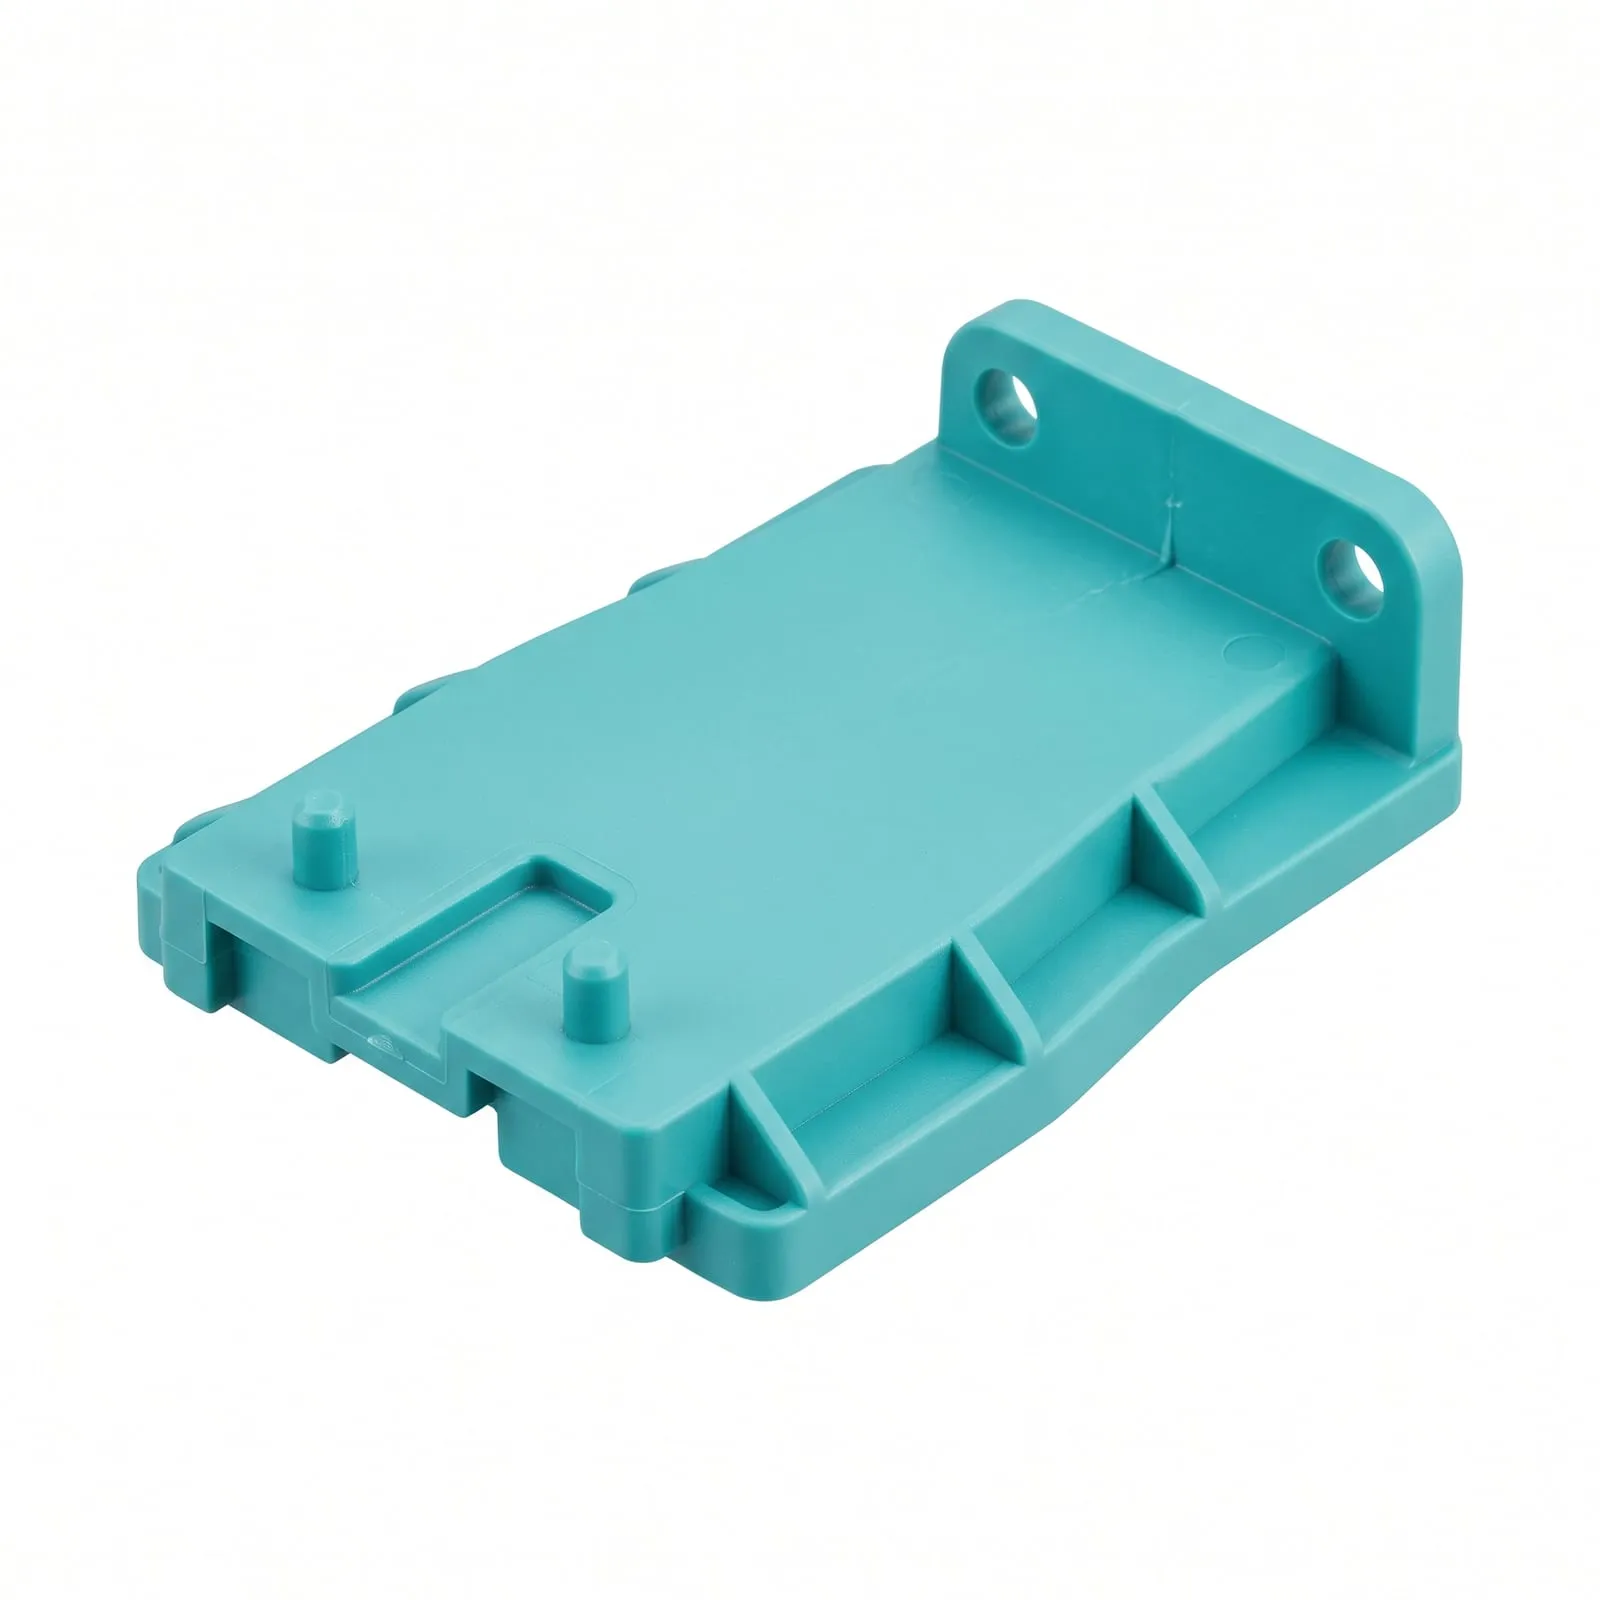
One mold can make a family of parts.
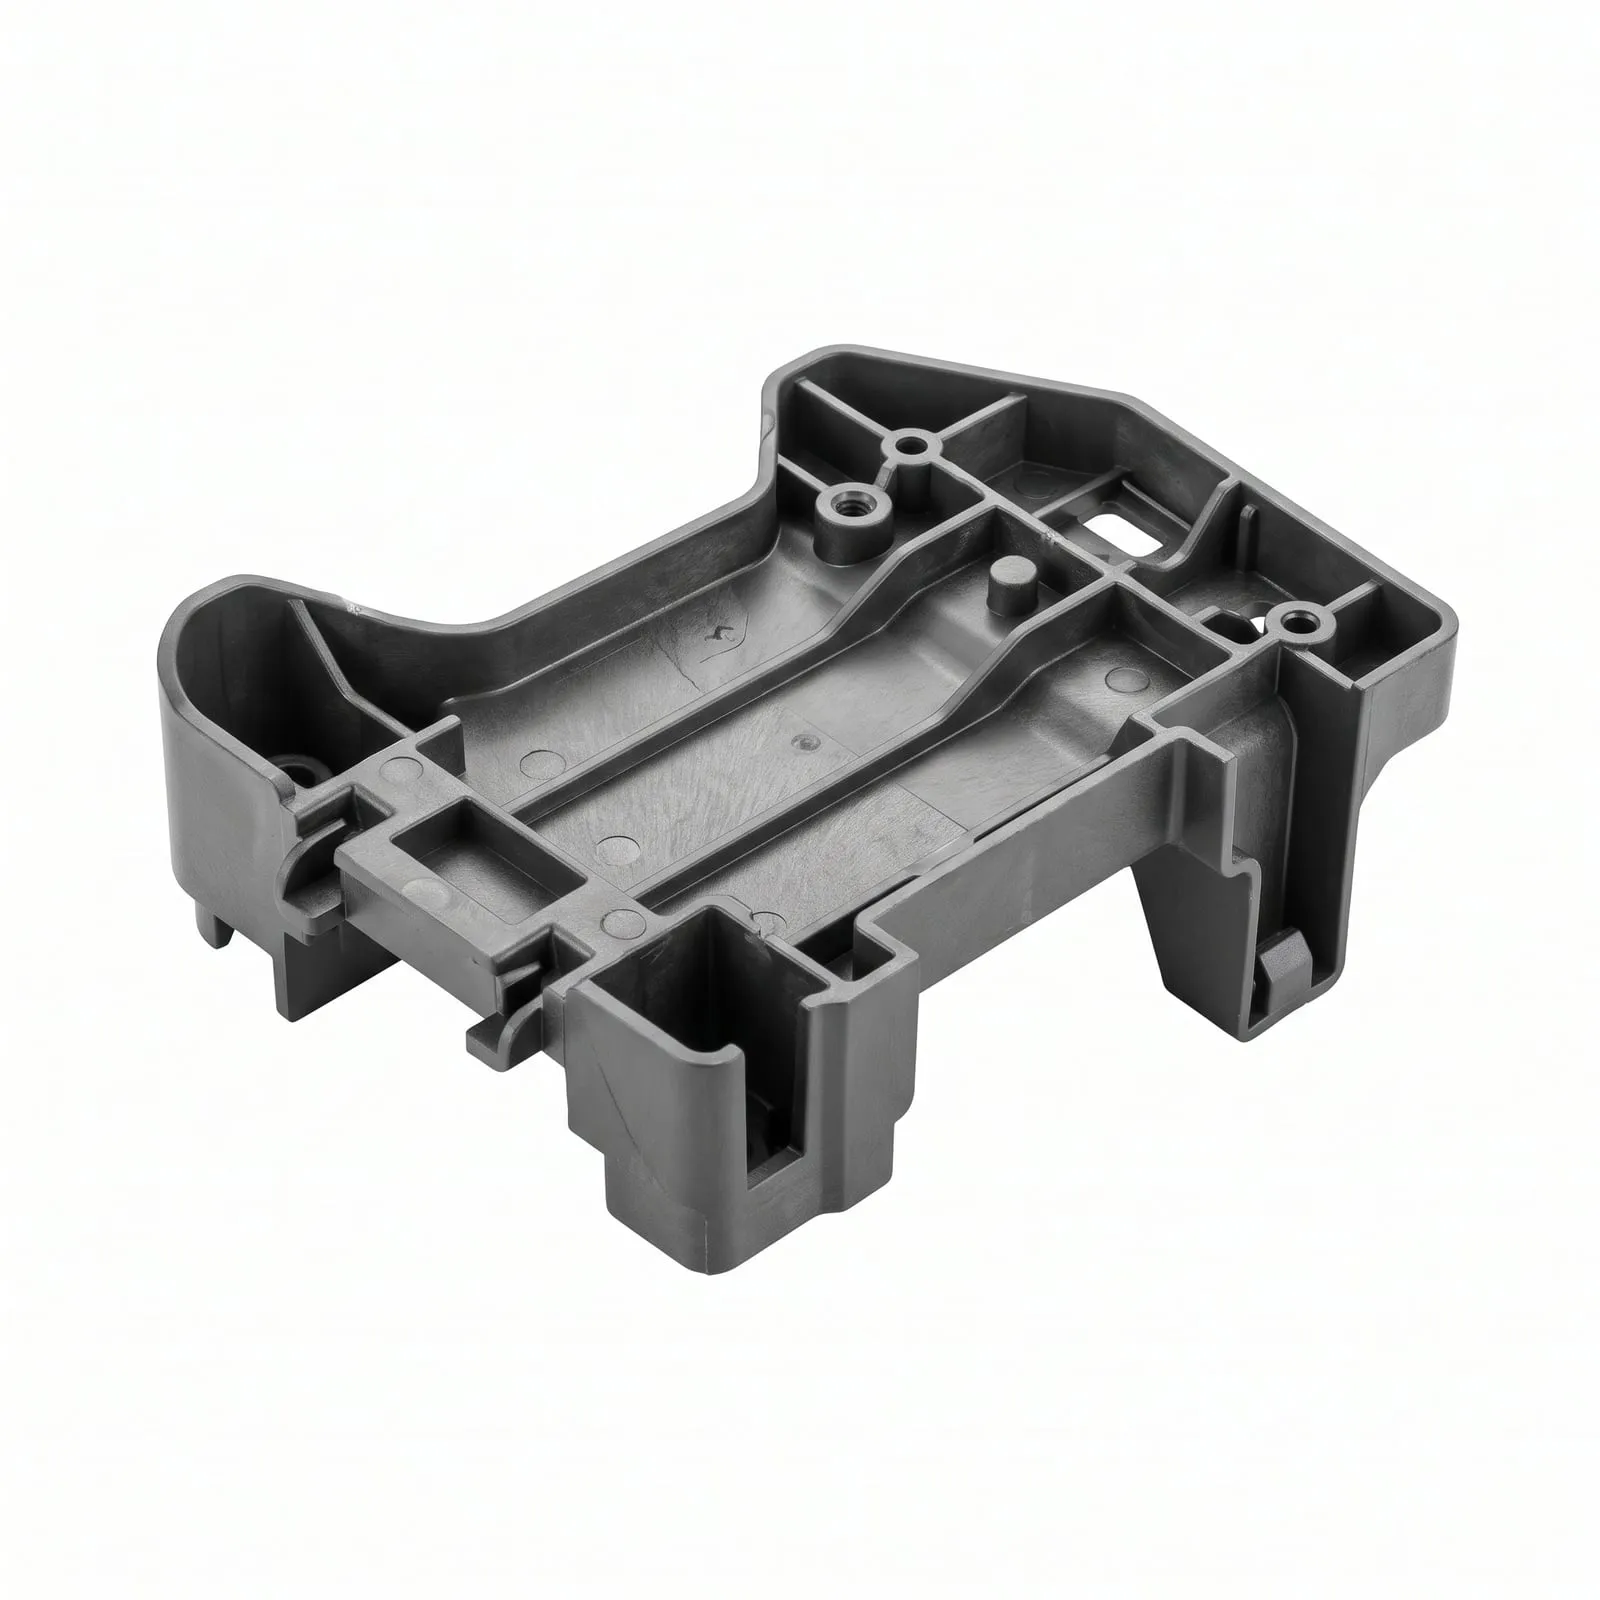
Several related parts share one mold and are priced together as a matrix, not as separate quotes. It suits parts sold in matched sets at similar volumes.
See how we build molds →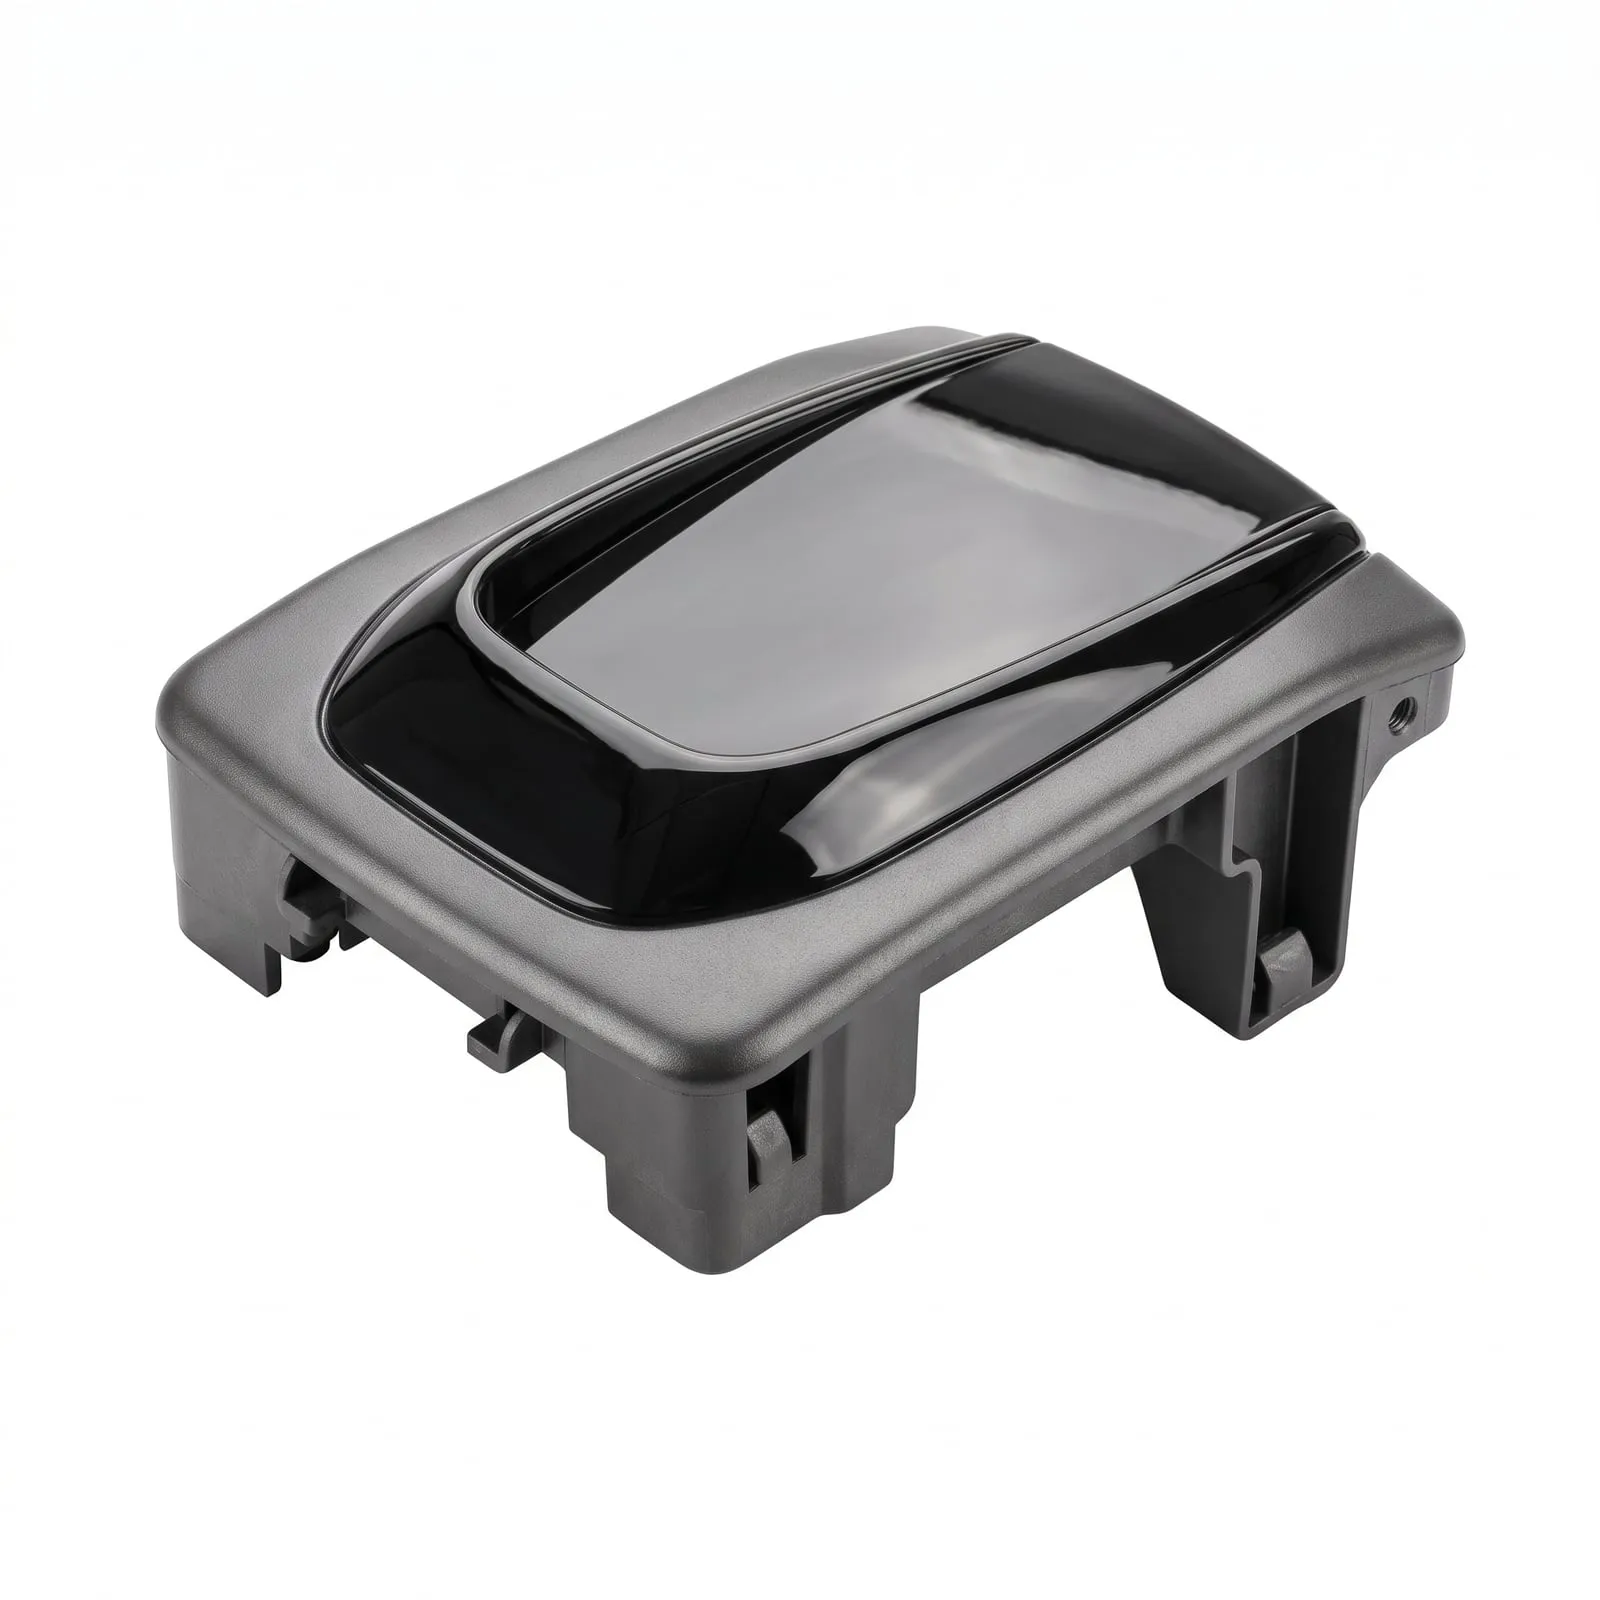
Family mold
1 tool · 4 cavities
- HousingHS-01
- Glossy trimTR-01
- BaseBS-01
- ClipCL-01
Beyond a single cavity
Specialized molding goes on the same quote.
Overmolding, inserts and finishes are planned into the tool, not added afterward.
Pick the tool your volume needs.
Aluminum is for validating the part and steel for production. We size the mold to the shots you will actually make.
Injection molding, defined
Injection molding is a manufacturing process where plastic resin is heated until molten, injected under pressure into a steel or aluminum mold, cooled and ejected as a finished part. It is the standard way to make identical plastic parts at volume — from a few hundred off a soft aluminum tool to millions off hardened steel.
What to send
What you send, and what you get back.
The 3D model and the PDF drawing are enough.
Your 3D model (STEP) and the 2D PDF drawing
The model gives the geometry; the drawing carries what the model cannot say: tolerances and critical dimensions. Material, colour, texture and quantity are chosen when you upload the part.
A price per part, in 24–48 hours
With the unit price and the lead time of every part; the tooling is shown apart when the part needs a mold.
If it can’t be molded as drawn, the change it needs
We tell you before anything is made, and requote it.
Not sure it's the right process yet?
Find your break-even before you talk tooling.
Interactive · rule of thumb
CNC or injection molding — where's your break-even?
CNC machining likely wins
At 251 units of a moderate part, mold tooling is hard to fully amortize — CNC keeps you off the hook for tooling cost and lead time.
Ballpark based on typical tooling payback — not a quote. The real number depends on your actual geometry, material and finish. Send the part for real numbers →
Everything about injection molding
Spec sheet
Resins
Choosing a process
Questions
Questions about injection molding
How much does an injection molded part cost?
You get a price per part, with the tooling shown apart when the part needs a mold. The unit price depends mainly on the size and wall thickness of the part, the resin, the number of cavities and the quantity: the more parts come off one mold, the less each one costs. Upload the STEP file and the 2D PDF drawing and you have the figure in 24–48 hours; asking for a quote commits you to nothing.
How much does an injection mold cost?
It depends on the size of the part, its geometry (undercuts add slides and lifters), the number of cavities, the surface finish and whether the mold is aluminum or hardened steel. Aluminum costs less and suits prototypes and bridge runs; steel costs more up front and is built for production. In the quote the mold is its own line, so you see what the mold costs and what each part costs.
Which files do I need to send?
The 3D model as a STEP file and the 2D drawing as a PDF. The model gives the geometry; the drawing carries what the model cannot say, such as tolerances, critical dimensions and surface finish. Material, colour, texture and quantity are chosen when you upload the part.
How long does the quote take?
Between 24 and 48 hours from the moment you upload the files, with a price per part and the lead time of each one. If the part can’t be molded as drawn, we tell you the change it needs before anything is made.
Can I order a single part, or only production runs? When does molding beat CNC?
We work from a single part to production runs. Below the quantity where a mold pays for itself, CNC machining is usually the better choice; above it, molding wins on price per part. Where that break-even sits depends on the part and the tool, and the break-even calculator on this page gives you a first idea. If your quantity doesn’t justify a mold, we say so and requote.
Can finishing, assembly and packaging go in the same order?
Yes. Pad printing, threaded inserts, overmolding and assembly are quoted and produced under the same order as the molding, and packaging can go in it too.
Where are the parts made, and is my design kept confidential?
Production is in Europe and Asia. A mutual NDA is in place before you upload any file.
Who owns the mold?
The mold is built for your part and it is yours; in the quote it appears as its own cost. It stays and runs in our shops and is not shipped, so every run comes from the tool you approved. If you need the terms on moving the mold, ask us before you accept the quote.
What's the real difference between a prototype mold and a production mold?
A prototype (or "bridge") tool is usually machined from aluminum — faster and cheaper to cut, good for anywhere from a few hundred to a few thousand shots before wear shows in cosmetic surfaces. A production tool is hardened steel (typically P20 or H13), costs more and takes longer to build, but is rated for hundreds of thousands of shots with tighter, more repeatable tolerances over the life of the tool.
What is a T1 sample, and what happens if it doesn't match the drawing?
T1 is the first set of parts pulled off a newly cut mold, measured against your drawing before the tool is signed off. If a dimension is out of spec, the tool gets adjusted — steel added or removed from the cavity — and re-sampled (T2, T3…) until it passes. Nothing ships to production on an unvalidated tool.
How many shots can a mold actually produce before it wears out?
It depends on the tooling material and the resin. Aluminum tools handle roughly hundreds to a few thousand shots before cosmetic wear; hardened steel tools are built for hundreds of thousands. Glass- or mineral-filled resins are abrasive and shorten cavity life faster than unfilled plastic, which is worth telling us before the tool is cut, not after.
Can a CNC-machined prototype go straight to a production mold without changes?
Rarely as-is. CNC tolerates sharp internal corners, zero-draft walls and certain undercuts that a mold can't release without extra tooling (slides, lifters) or a redesign. The geometry usually needs a draft-angle and wall-uniformity pass first — see the DFM guide, or send the CNC file and we will flag exactly what needs to change.
My part was designed for 3D printing — can it be injection molded?
Usually yes, after an adaptation pass. Printing tolerates geometry a mold can't fill or release — sharp internal corners, uneven walls, solid sections, undercuts — so a print-ready file rarely molds as drawn. Send it anyway: we price it for molding and flag that it'll need adapting; once you approve the quote, the DFM pass reworks the geometry with you — draft angles, uniform walls, ribs instead of solid volume — alongside the mold makers who'll actually build the tool, and the part still works and looks the way you designed it. And if your volume doesn't justify tooling yet, we'll say so and quote a printed batch or urethane casting instead.
What's a family mold, and when does it make sense?
A family mold cuts several different part cavities into one tool, so they run — and ship — together. It's cost-efficient when the parts are used in matched sets and need similar volumes, the way a housing, its trim and its clips share one tooling strategy. The tradeoff: if one cavity wears or breaks, the whole set is held up until it's fixed.
Why do parts warp or show sink marks after molding, and do I need to redesign the whole part?
Both are usually a wall-thickness problem, not a whole-part problem. Sink marks show up opposite a rib, boss or thick section that cools slower than the wall around it; warping comes from uneven cooling or fiber orientation in glass-filled resin. The fix is almost always local — thin a rib, add cooling near a thick section — rather than a ground-up redesign.
What if injection molding isn't the right process for my part?
Then it changes — before any tooling is cut. If your volume is too low to justify a mold, or your geometry fits CNC or sheet metal better, we say so upfront and requote under the right process. Asking for a quote commits you to nothing.
Related capabilities
Get started
Upload your part and get its quote.
Upload one part or your whole BOM.
You get a price and lead time in 24–48 h.
Your parts protected by an NDA.